Toolpaths from the part, held to the machine.
The feeds come from the tool, the material and the machine's ceilings. A flat outline is planned here in milliseconds; a solid goes to FreeCAD's Path.
Case study 1 · the speed and the feed
The spindle is the limit, so the feed follows it.
UpperBody-001's lamp plate is 92 × 46 × 3 mm of aluminium. The fleet's 3018 routers carry a 180 W spindle. Its kit page gives 7,000 rpm at 24 V, which no unit has measured. Aluminium wants a faster spindle, so the feeds engine ran it at that ceiling and worked the feed out from it, keeping the chip load.
The engine also said what a machinist would: a full-width slot has nowhere for its chips to go, so take a lighter depth than a profile pass, or cut it trochoidally.
- , held at the machine's ceiling
- 7,000 rpm
- feed for a 3.175 mm two-flute end mill
- 370 mm/min
- chip per tooth
- 0.026 mm
- of cutting power, of the spindle's 180 W
- 4.7 W
cloud://home/user-commandagi/case-studies/cam/lamp-plate-feeds.call.jsonEjecución runs/20261107t113132z-lamp-plate-feedsHerramienta fab_feedsSe ejecutó en This computer (dell-gb10-1)Cuándo Case study 2 · the outline and the holes
Ten passes, four tabs to hold the part.
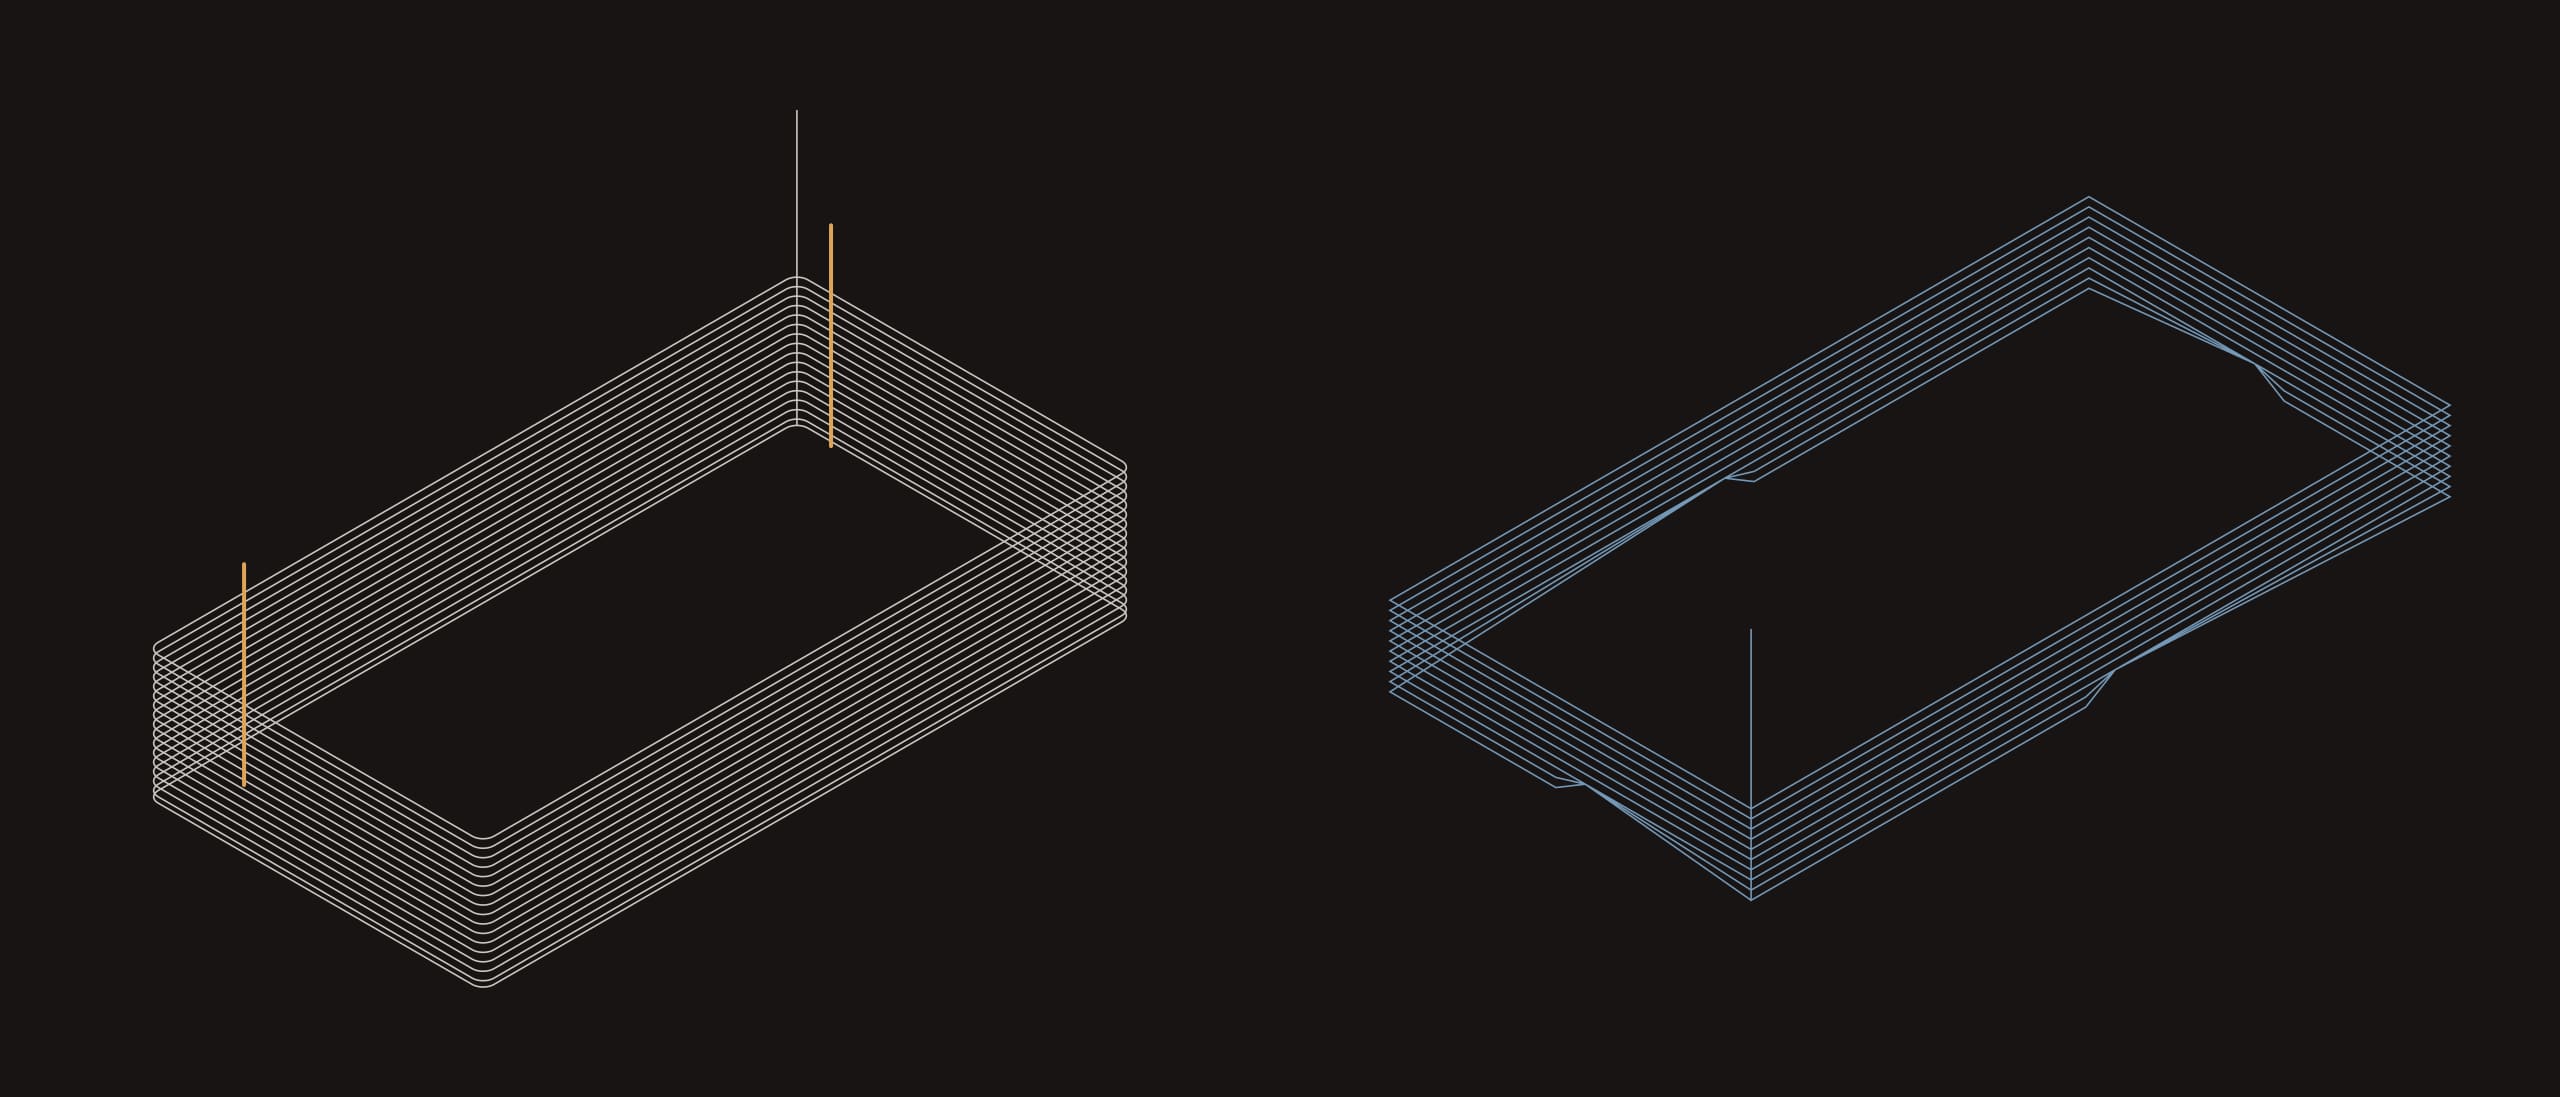
On the right, fab_mill_region cut the outline free in 0.3 mm passes and left four tabs, so the plate does not come loose into the cutter on the last pass. On the left, FreeCAD's Path contoured and drilled the same plate from the module's own solid in Body.3d.tsx. The picture draws the depth four times its size, from runs 20261107t113120z-lamp-plate-contour, 20261107t113126z-lamp-plate-drill and 20261107t113136z-lamp-plate-profile.
- passes through 3 mm
- 10
- of cut, about 7.8 min at 370 mm/min
- 2,887 mm
- tabs, holding 16 mm of the outline
- 4
- holes of Ø3.4, pecked 0.5 mm at a time
- 2
cloud://home/user-commandagi/case-studies/cam/lamp-plate-profile.call.jsonEjecución runs/20261107t113136z-lamp-plate-profileHerramienta fab_mill_region (the picture also draws the drill run 20261107t113126z-lamp-plate-drill)Se ejecutó en This computer (dell-gb10-1)Cuándo What the machine would get
Two programs for grbl, zeroed at the stock's corner.
The contour and the drilling are each one program, posted for the grbl controller of the 3018. The plate sits at Z 532 mm in the module's assembly, so the export moves each program to the stock's own origin: X0 Y0 Z0 is the stock's low corner, and the program's first line says where that corner was in the part's frame (X37.000 Y61.700 Z531.950). The stock is the plate with 5 mm past it on each side. Both programs are then held to the 3018's 300 × 180 × 45 mm envelope. Every program says unvalidated: no part has been cut with it on a real machine, and sending it to one is a separate, granted act. Not fabrication-ready.
The first run of this case failed, and said so: with the stock the size of the plate, the contour's tool centre ran 1.59 mm outside it, to X −1.587, and the envelope check refused the program. The cause was that the route knew no stock beyond the part. It now takes the stock's margin (stockMargin).
- lines in the contour program, from X 3.4 to 98.5 mm, Y 3.4 to 52.6 mm and Z −1 to 9 mm
- 201
- lines in the drilling program, from X 8.0 to 94.0 mm and Z 0 to 9 mm
- 123
- of stock past the plate on each side
- 5 mm
- of the fleet's routers commissioned
- 0
cloud://home/user-commandagi/case-studies/cam/lamp-plate-contour.call.jsonEjecución runs/20261107t113120z-lamp-plate-contourHerramienta fab_cam: FreeCAD Path in cam-eval, grbl postSe ejecutó en This computer (dell-gb10-1)Cuándo Plan a cut on your machine.
Name the tool, the stock and the machine. An agent plans the path and says when a number would break a tool.